Download IVISION Catalog

 01
Define the visible criteria
Agree which part conditions are observable and relevant.
A supported visual check can flag an unexpected chip, deformation or other validated appearance anomaly on a part. Inspectors must confirm the condition against the specification and use appropriate methods for hidden or functional defects.
Confirm detector support, camera suitability and the proposed event workflow before deployment.
Validate part anomaly inspection
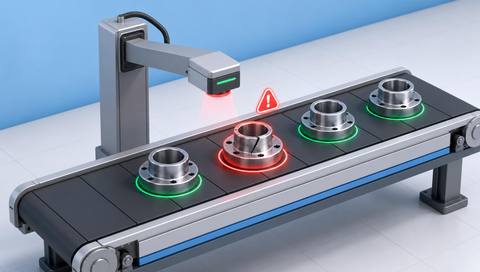
 Without IVISIONStandard CCTV feed
 With IVISIONIllustrative event overlay
The Process
Focus inspection on the surface and features in view Help inspectors focus on parts that need a closer quality check.
01Agree which part conditions are observable and relevant.
 02
Test acceptable variation and known visible defects.
 03
Inspect the image and trace the candidate to the physical part where supported.
 04
Qualified staff use the specification and required tests.
Explore Your Options
| Dimension |  Defective-part detection |  Surface-defect detection |
|---|---|---|
| Observation |  Visible part features that differ from validated acceptable examples. | Visible scratches, blemishes or finish irregularities in the inspected area. |
| Event criteria | A supported anomaly or defect-class observation meets the agreed review criteria. | A supported surface condition differs from the validated acceptable reference. |
| Monitoring setup | Define defect classes, acceptable variation and part presentation. | Specify surface types, defect examples and acceptable variation. |
| What it cannot establish | Video does not reveal every internal defect, dimensional error or functional failure. | Video does not establish defect depth, material integrity or hidden subsurface flaws. |
| Practical outcome | Help inspectors focus on parts that need a closer quality check. | Help inspectors locate surface conditions requiring comparison with the finish specification. |
Illustrative demonstration
Example footage and simulated events explain the review workflow. They do not measure detector performance.
 Sites overview
No matching events.
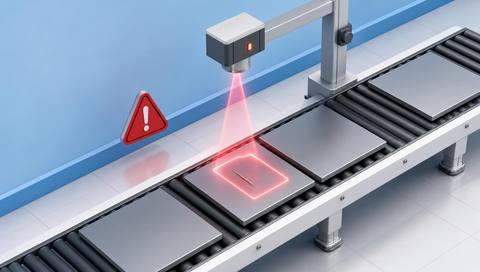 Production Monitoring
Focus on visible surface marks and finish conditions.
Read More
 Production Monitoring
Place the visual check within broader quality criteria.
Read More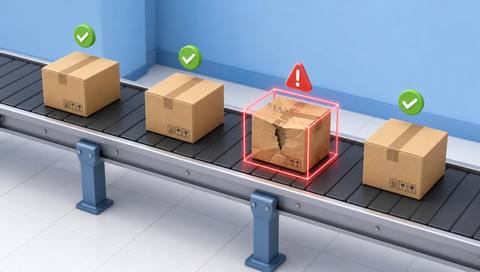 Production Monitoring
Review the finished item after assembly or processing.
Read MoreEXPLORE WHAT’S POSSIBLE
01 / 04 · DEFECTIVE-PART DETECTION
Visible edge damage needs checking before use.
Example event: A candidate chip appears on the inspected part.
Operator response: Examine the part against acceptance criteria.
Practical value: Focus an incoming-quality check.
Discuss this capability02 / 04 · DEFECTIVE-PART DETECTION
Molded parts can show visible deformation.
Example event: A supported appearance check flags an anomaly.
Operator response: Verify the condition and process context.
Practical value: Support review before assembly.
Discuss this capability03 / 04 · DEFECTIVE-PART DETECTION
Surface damage may be overlooked in a tray.
Example event: A visible blemish is identified for review.
Operator response: Inspect the cover under approved lighting.
Practical value: Direct attention to the relevant feature.
Discuss this capability04 / 04 · DEFECTIVE-PART DETECTION
Show the relevant part surfaces at adequate resolution.
Visibility: Hidden faces, reflections and fine defects may be missed.
Configuration: Validate each defect class and acceptable variation on real parts.
Privacy: Limit retained images to the quality and traceability purpose.
Human review: Inspectors determine acceptance using the full specification.
Discuss this capabilityFrequently asked questions
Identify candidate visible anomalies on individual parts before assembly or further processing.
No. Only validated visible conditions are within scope.
Not unless they produce visible evidence; other inspection methods may be needed.
Dimensional inspection requires a separately calibrated method.
Traceability requires a verified identification and record connection.
Find your fit
Help inspectors focus on parts that need a closer quality check. For Incoming quality inspectors, Component manufacturing teams.
Workflow to discuss
Defective-part detection + Focus inspection on candidate visible anomalies.
Discuss a camera view, a monitoring question and the review process your team needs.